6 Key Benefits of Legacy PLC Migration for UK Manufacturers: Operational ROI & Risk Mitigation
Operating obsolete programmable controllers like Allen-Bradley SLC 500 or Siemens S5 is a ticking operational timebomb. Discover how UK engineering directors eliminate catastrophic obsolescence, slash unplanned downtime, protect facilities against cyber threats, and unlock smart factory data.
Executive Summary: The Cost of Doing Nothing
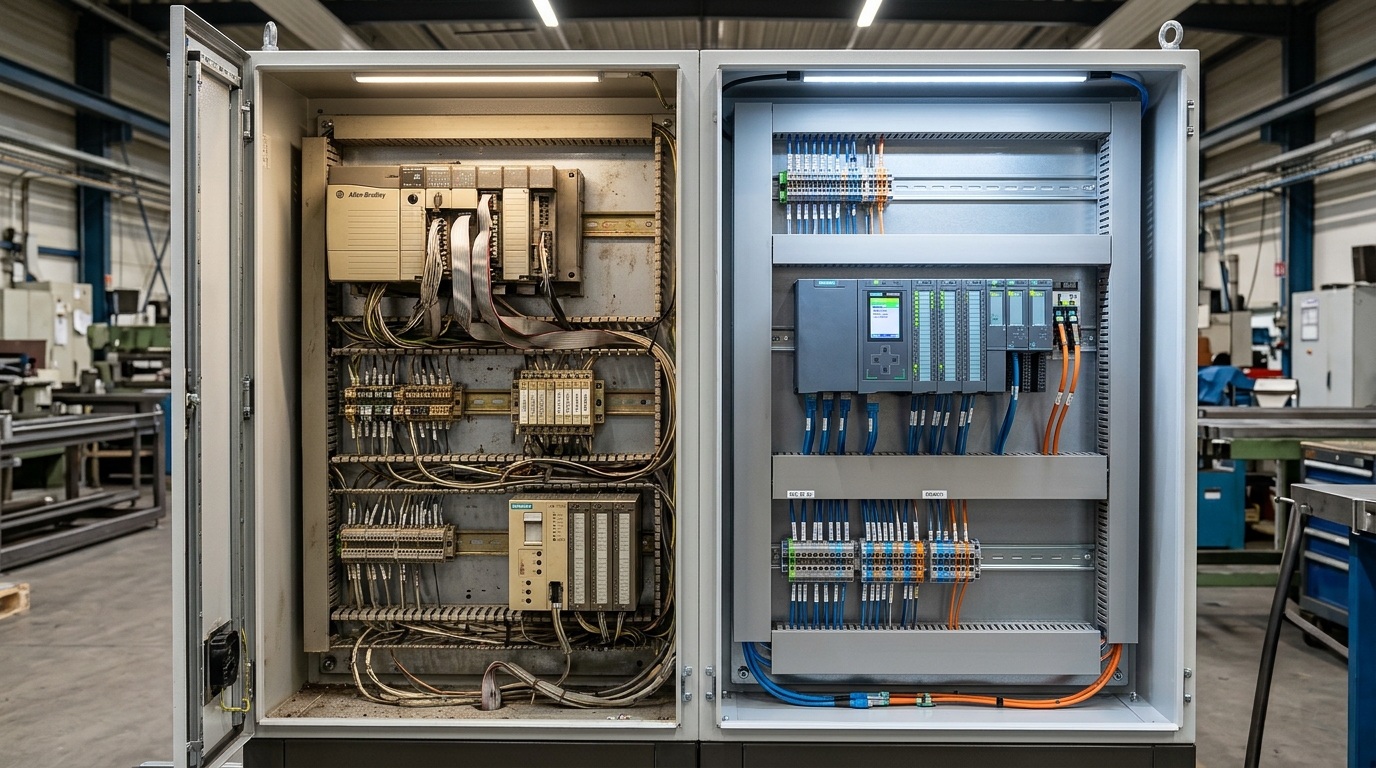
Across British manufacturing facilities in automotive, food processing, chemicals, and pharmaceuticals, thousands of critical production lines still run on legacy controllers installed between 1995 and 2008. While these systems once proved indestructible, OEM end-of-life notices have transformed them into high-stakes operational risks.
When a legacy CPU, power supply, or analog card fails today, plants no longer face a routine maintenance fix. They face emergency secondary broker auctions, counterfeit electronic components, astronomical downtime costs (£10,000 to £85,000+ per hour), and insurers questioning OT safety compliance. Proactive PLC migration is no longer an optional capital project; it is an existential business continuity imperative.
Eliminate Obsolescence Risk & Grey-Market Component Scarcity
The primary catalyst for PLC migration across UK manufacturing is hardware obsolescence. Global automation vendors such as Siemens, Rockwell Automation (Allen-Bradley), Mitsubishi Electric, and Schneider Electric enforce disciplined product lifecycles. Once a platform enters "Discontinued" or "Silver Series" status, factory spare manufacturing ceases permanently.
- Rockwell Automation: SLC 500, PLC-5, MicroLogix 1000/1200/1500, PanelView Standard.
- Siemens: SIMATIC S5 (100U/115U/135U/155U), S7-200, early S7-300/400.
- Mitsubishi Electric: MELSEC A-Series, FX1N, FX2N, AnS micro PLCs.
- Schneider / Modicon: TSX Quantum, TSX Premium, Micro 07 series.
- Omron: Sysmac C200H, C1000H, CQM1, CPM2A series.
Relying on legacy hardware forces engineering managers into a dangerous dependence on secondary brokers and refurbished online sellers. This creates three acute business liabilities:
Obsolete analog cards and power supplies regularly command 500% to 1,200% over original catalog list prices as global stocks shrink.
Used cards sourced from overseas dismantlers carry aged electrolytic capacitors, thermal solder fatigue, and zero OEM warranty.
When an unstocked I/O card burns out, sourcing an identical replacement can take 4 to 12 weeks, during which your line sits completely halted.
By executing a planned modernization to active architectures like Siemens SIMATIC S7-1500 or Allen-Bradley ControlLogix 5580, your plant benefits from guaranteed 10 to 15-year active commercial support, off-the-shelf distributor availability, and full manufacturer warranty.
Mitigate Crippling Unplanned Downtime & Preserve Revenue
Unplanned downtime is the single greatest destroyer of manufacturing gross margin. In UK food and beverage processing, high-speed packaging, tier-1 automotive manufacturing, and continuous chemical batch operations, an unscheduled stoppage causes immediate financial losses:
When a legacy controller crashes, fault-finding is notoriously sluggish. Engineers must search for vintage laptops running Windows 98 or XP, connect through fragile RS-232 serial adapters, and navigate archaic ladder logic without descriptive rung comments.
In contrast, modern automation systems incorporate onboard web servers, granular diagnostic buffers, and millisecond-accurate timestamping. When a field sensor faults or an MCC contactor trips, modern controllers instantly report the exact channel, device tag, and failure condition directly to the HMI or remote engineering smartphone, turning hours of forensic searching into a 5-minute component swap.
Hardened OT Cybersecurity & Compliance with UK NIS Regulations
When legacy PLCs were engineered in the 1990s, plant floors were completely isolated from corporate IT networks and the internet. Today, operational technology (OT) is interconnected with manufacturing execution systems (MES), ERP databases, and remote vendor diagnostics.
Controllers like Rockwell SLC 500 or Siemens S5 lack fundamental security controls. Any device on the factory network can overwrite registers, force I/O bits, copy proprietary recipe logic, or upload corrupt bytecode without password authentication or cryptographic verification.
Major UK industrial insurance underwriters increasingly audit factory OT environments before renewing business interruption coverage. Migrating to modern secure controllers guarantees compliance with cybersecurity mandates and prevents ransomware from spreading across production equipment.
Unlock IIoT, Real-Time OEE Metrics & Seamless SCADA Integration
Data is the cornerstone of modern industrial optimization. Continuous improvement managers depend on Overall Equipment Effectiveness (OEE) tracking, predictive vibration analysis, and energy monitoring to stay competitive.
Legacy controllers isolate this data in proprietary silos. Protocols such as Allen-Bradley Data Highway Plus (DH+), Remote I/O (RIO), Siemens PROFIBUS DP, or Modbus RTU communicate at slow serial speeds and cannot publish data directly to IP-based plant dashboards without clunky hardware protocol gateways.
Modern Fieldbus & Cloud Edge Connectivity
Modern PLC processors include native multi-port gigabit Ethernet, supporting PROFINET, EtherNet/IP, Modbus TCP, OPC UA, and lightweight MQTT. Controllers publish live cycle times, reject counts, motor torque profiles, and thermal metrics directly to SQL historians, Ignition SCADA, or cloud IoT dashboards without third-party converters.
Explore how MASK Control Systems integrates live telemetry into modern systems via our specialized Systems Integration Services and secure Remote Monitoring Solutions.
Boost Motor Efficiency & Reduce Industrial Carbon Footprint
With UK industrial electricity tariffs remaining high, energy consumption represents one of the largest controllable operating expenses. Vintage control cabinets frequently run motors via direct-on-line (DOL) contactors or antiquated star-delta starters that draw heavy inrush currents and run fans and pumps at constant 100% speed.
Modern PLCs coordinate networked Variable Speed Drives (VFDs) to match exact real-time process demand, slashing motor electricity consumption by 20% to 45% under Affinity Law physics.
Integrated smart energy transducers feed real-time kWh metrics per manufactured batch directly into plant management reporting, satisfying UK Streamlined Energy and Carbon Reporting (SECR) legal mandates.
To guarantee electromagnetic compatibility and protect digital instrumentation from high-frequency noise during drive upgrades, consult our engineering guide on VFD EMC Noise Mitigation & Shielding.
Overcome Retiring Engineering Skill Gaps & Tooling Friction
The UK manufacturing sector faces a well-documented engineering demographic shortage. The generation of controls engineers and electrical technicians who mastered DOS-based programming, custom serial pinouts, and obsolete instruction sets (such as STEP 5 Statement List or RSLogix 500 memory addressing) are rapidly retiring.
Modernizing to standard IEC 61131-3 platforms expands your engineering support talent pool exponentially. Any competent modern controls engineer or certified systems integrator can connect via standard laptops, run diagnostics, adjust code, or deliver secure remote VPN assistance within minutes.
Total Cost of Ownership (TCO): Retaining Legacy vs Modern Migration
Evaluating an automation upgrade requires looking beyond initial capital expenditure (CapEx) to consider cumulative operating expenditures (OpEx) and catastrophic downtime risks over a 5-year operating window:
| Operational Category | Retaining Legacy PLC System | Modernized MASK Architecture |
|---|---|---|
| Spare Parts Sourcing | Unregulated brokers, 500% to 1000% markups, 4 to 12 week lead times | Off-the-shelf UK stock, next-day delivery, standard list pricing |
| Cybersecurity & Compliance | Unencrypted plaintext, no access logs, high insurance audit non-compliance risk | Hardware secure-boot, encrypted TLS / CIP Security, IEC 62443 aligned |
| Mean Time to Repair (MTTR) | 4 to 16 hours (manual multimeter tracing, missing ladder comments) | 15 to 30 minutes (plain-text HMI alarms, web server diagnostics) |
| Engineering Support Access | Shrinking pool of semi-retired contractors charging premium emergency callout rates | Vast national pool of qualified engineers, full unencrypted open code ownership |
| Factory Data & Analytics | Isolated serial silos, manual paper clipboards, no live OEE metrics | Native OPC UA / MQTT, automated real-time cloud SCADA & ERP reporting |
| Safety System Integration | Complex discrete safety relays requiring extensive interlock rewiring | Integrated Fail-Safe Safety PLC (SIL3 / PLe) over safety fieldbus |
Table 1: 5-year Total Cost of Ownership comparison between obsolete legacy controllers and modern industrial automation infrastructure.
How MASK Control Systems Executes Zero-Downtime Cutover
The primary concern voiced by plant directors is the fear of prolonged production stoppage during site cutover. At MASK Control Systems Ltd, our phased migration methodology guarantees seamless execution:
We extract your existing program, resolve obsolete timer formats and indirect memory registers, and convert the logic into clean, modular IEC 61131-3 code with full tag documentation.
Before visiting your plant, the complete hardware rack is tested at our UK workshop against simulated I/O, emergency stops, and SCADA communication, achieving 100% logic verification prior to dispatch.
Where existing field wiring is intact, we design pre-wired harness adapters or custom 3D CAD backplates that drop directly into the footprint of your old rack, avoiding days of field termination tracing.
Physical cutover is scheduled during standard 24 to 48-hour weekend windows. Our senior automation engineers remain on site for first-production shift support, ensuring smooth Monday startup.
For an in-depth technical walkthrough on step-by-step conversion techniques for SLC 500 and Siemens S5, explore our companion technical guide: Legacy PLC Migration Strategy & Implementation.
Frequently Asked Questions: Legacy PLC Migration
What are the main financial risks of delaying a legacy PLC migration?
Can an existing control panel enclosure be retained during a PLC upgrade?
How does legacy PLC migration resolve OT cybersecurity risks and NIS2 regulations?
What cutover strategies guarantee minimal factory downtime during migration?
Which legacy PLC platforms are most urgent for migration in UK factories today?
Does MASK Control Systems provide full software ownership after migration?
Plan Your UK Factory PLC Migration with MASK Control Systems
Protect your plant against catastrophic obsolescence and unbudgeted downtime. Our Devon and UK-wide controls engineering team provides comprehensive plant audits, digital twin simulation, and rapid turnkey cutover.