Commercial Packaging & Cartoning Automation: Delta Robot Pick-and-Place, Case Erectors & PackML Line Synchronisation
Engineered for UK food processors, pharmaceutical contract packers, and FMCG manufacturers. MASK Control Systems Ltd delivers bespoke packaging control panels, high-speed multi-axis delta robot cells, automated case erectors, machine vision inspection, and deterministic PackML line balancing that eliminate end-of-line bottlenecks.
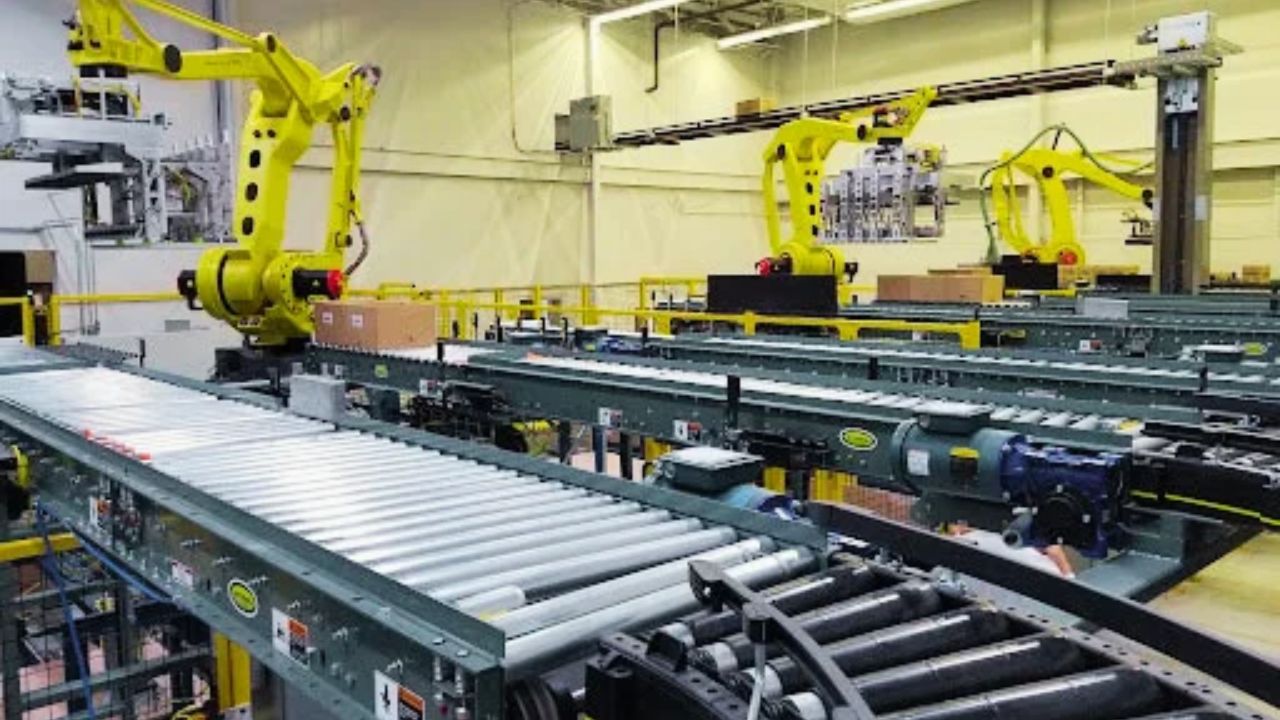
Turnkey packaging control panels engineered in Cullompton, Devon.
Eliminating Packaging Bottlenecks and Accelerating Line Throughput
In modern FMCG and manufacturing facilities, the packaging hall represents the most vulnerable link in the production chain. Even if upstream cooking, baking, or assembly runs at 100% capacity, an uncoordinated cartoner, an uncalibrated optical vision sensor, or manual case packing creates severe backpressure that halts the entire plant.
Headquartered in Cullompton, Devon, MASK Control Systems Ltd bridges the gap between mechanical packaging machines and high-speed multi-axis digital control. We design, program, and commission bespoke electrical control panels for delta robot pick-and-place skids, continuous cartoning machines, automated case erectors, vision inspection tunnels, and downstream checkweighing stations across the UK.
Turnkey Engineering for Primary, Secondary & End-of-Line Packaging
From high-speed robotic sorting to corrugated case packing and validation, our engineering team deploys deterministic, low-maintenance automation:
Delta Robot High-Speed Pick-and-Place
Kinematic delta robot motion control with real-time conveyor tracking. Interfaces with upstream optical 2D vision cameras to pick randomly positioned pouches, bottles, or snacks from continuously moving belts at up to 180 cycles per minute into carton pockets.
Continuous & Intermittent Cartoning
Electronic camming replacing complex mechanical linkages. Controls rotary carton blank extraction, barrel loader pusher synchronization, leaflet inserter interlocks, and Nordson hot-melt adhesive glue pattern verification with zero carton loss.
Machine Vision Inspection & Reject Gates
Cognex and Keyence high-speed line scan and area cameras. Inspects 1D/2D barcodes, expiry date OCR/OCV verification, label presence and skew, and seal integrity, triggering pneumatic reject cylinders with millisecond timing accuracy.
Automated Case Erectors & Tray Formers
Pneumatic vacuum arm blank pull-down, positive case squaring mechanisms, and bottom flap tucking. Features magazine low-blank sensors, automated tape break detectors, and high-speed servo pushers feeding case packing stations.
PackML Multi-Machine Line Balancing
Standardized OMAC Packaging Machine Language state models across upstream flow-wrappers, cartoners, and case packers. Dynamically throttles conveyor speeds based on buffer accumulation, eliminating sudden stops and line surges.
Checkweighing & Metal Detection Feedback
In-line dynamic load cell checkweighing compliant with UK Weights and Measures average weight system. Features automatic feedback loops that adjust upstream filling pistons, plus fail-safe locked reject bins for contaminated packs.
ISO 13849-1 PLe Functional Safety & Machine Safeguarding
High-speed packaging machinery combines powerful servo actuators, rapid pneumatic cylinders, and rotating carton chains. Maintaining high operational throughput requires safeguarding that protects operators without causing unnecessary line nuisance trips.
MASK Control Systems designs safety systems conforming to the highest international machinery directives:
- Optical Safety Light Curtains with Muting: Type 4 light curtains placed at carton infeed and outfeed openings with timed sequential sensor muting, allowing boxes to pass while stopping robot kinematics if operators reach in.
- Integrated Safety PLCs: GuardLogix and Siemens F-CPUs managing safety zones independently, allowing safe jam clearing on one section while adjacent machines remain in standby.
- Safe Torque Off (STO) & Safe Stop 1 (SS1): Direct digital safety integration to servo drives, guaranteeing torque removal in milliseconds without mechanically wear-inducing emergency brakes.
Packaging Compliance & Standards Matrix
Highest level functional safety architectures for high-speed delta robots and continuous cartoning lines.
Uniform state models that eliminate control incompatibility across multi-vendor packaging machines.
EMC shielded servo cables, low-voltage control circuits, and vibration-resistant spring-clamp terminals.
Digital audit logs, fail-safe bin status confirmation, and automated rejection records.
Motion Controllers, Servo Drives & OEE Dashboards
We engineer scalable automation platforms tailored to UK packaging lines, choosing the optimal silicon architecture for high-speed multi-axis motion:
Siemens SIMATIC S7-1500T
Technology CPUAdvanced multi-axis kinematics and electronic gearing. Directly coordinates delta robot axes, rotating carton knife blades, and continuous infeed flight lugs over PROFINET IRT with sub-microsecond jitter.
Rockwell Kinetix 5700
CIP MotionGuardLogix 5580 paired with dual-axis Kinetix servo drives. High-density shared DC bus architecture reduces cabinet heat dissipation and simplifies multi-axis carton pusher synchronization.
Real-Time Line OEE
Ignition & FT ViewReal-time touchscreen dashboards tracking cartons per minute, rejection breakdown categories (barcode failure, low weight, flap open), and automated micro-stop loss analysis.
Frequently Asked Questions: Packaging Automation
Key questions asked by UK packaging operations directors, project engineers, and co-packers:
How does conveyor belt tracking work with delta robot pick-and-place cells?
What is PackML and how does it prevent line blockages across packaging machinery?
What safety level is required for robotic cartoning and automated case erecting cells?
Can your vision systems perform barcode grading and optical character verification (OCV)?
How do you handle rapid SKU recipe changeovers on automated cartoning lines?
Upgrade Your Packaging Line Speed, Accuracy & PackML Synchronisation
Discuss your robotic pick-and-place cell, cartoning retrofit, automated case erector, or vision inspection upgrade with our senior automation engineers. We deliver bespoke electrical designs, proven PLC/motion software, and seamless on-site commissioning across the UK.