ABB PLC Programming & AC500 Automation Systems
Expert ABB AC500, AC500-eCo, and AC500-XC extreme condition PLC programming, Automation Builder software engineering, AC500-S functional safety integration, and CP600 HMI design delivered across the UK and worldwide.
Scalable Industrial Automation Built for Demanding Environmental Conditions
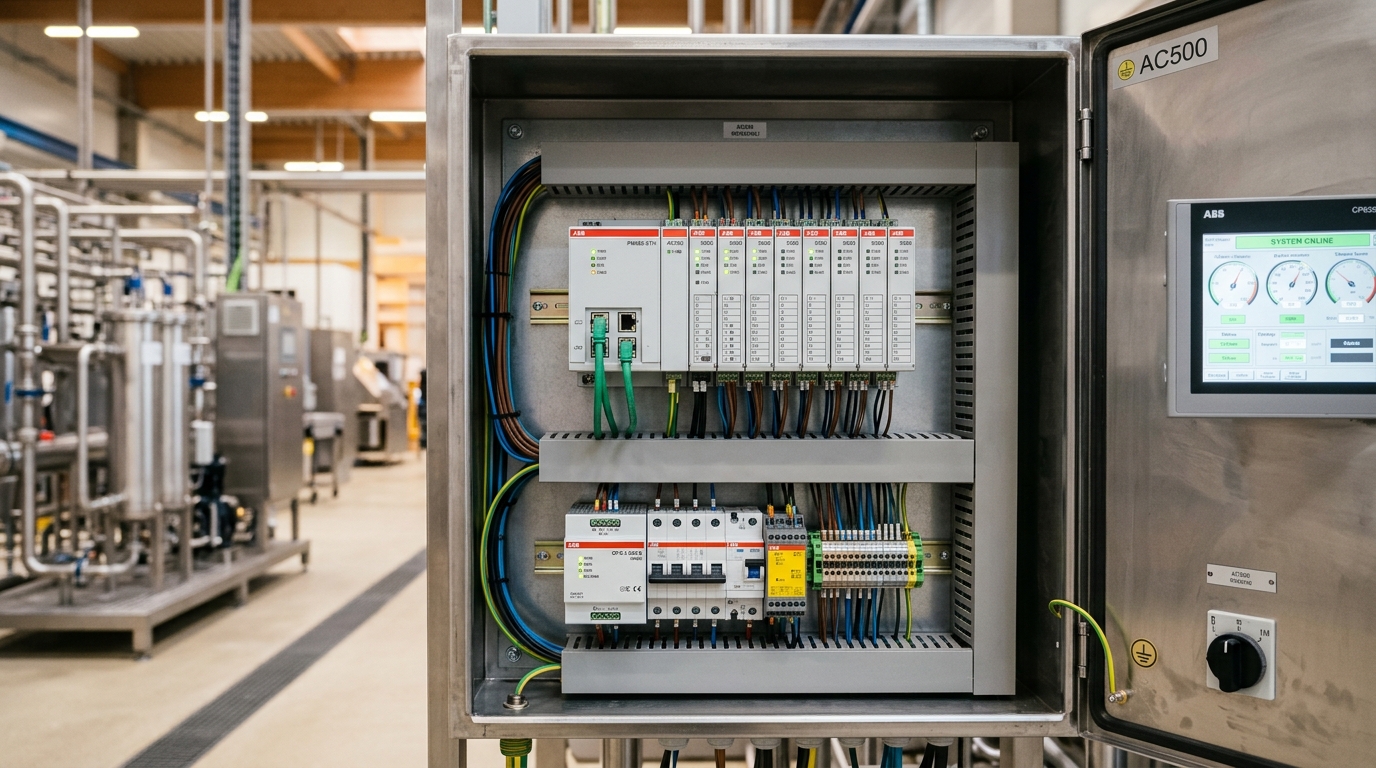
ABB programmable logic controllers represent a benchmark in industrial automation versatility, combining modular hardware scalability with uncompromising environmental ruggedness. From standard manufacturing plant floors to sub-zero cold storage facilities, municipal water networks, and offshore marine installations, the ABB AC500 platform delivers reliable deterministic control where other systems falter.
At MASK Control Systems, our senior controls engineers provide complete turnkey engineering across the ABB automation ecosystem. Utilizing ABB Automation Builder, we design, program, build, and commission custom control solutions. Whether you require modular AC500 V3 controllers, extreme-condition AC500-XC hardware for harsh atmospheric environments, or certified AC500-S functional safety logic, our systems are engineered for continuous operational uptime.
The scalable industrial controller for demanding manufacturing machinery, high-channel-count distributed I/O, and complex process automation lines.
Engineered specifically for operating environments where standard commercial PLCs fail due to severe cold, extreme heat, shock, or corrosive atmospheres.
Economical, standalone micro-controllers designed for smaller automated machines, packaging stations, and dedicated pumping or HVAC skids.
Dual-processor safety controllers certified to the most stringent international standards for cranes, hoists, presses, and safety-critical machinery.
Our ABB PLC & AC500 Engineering Services
From fresh Automation Builder software development and extreme-condition control panels to multi-protocol telecontrol and certified functional safety.
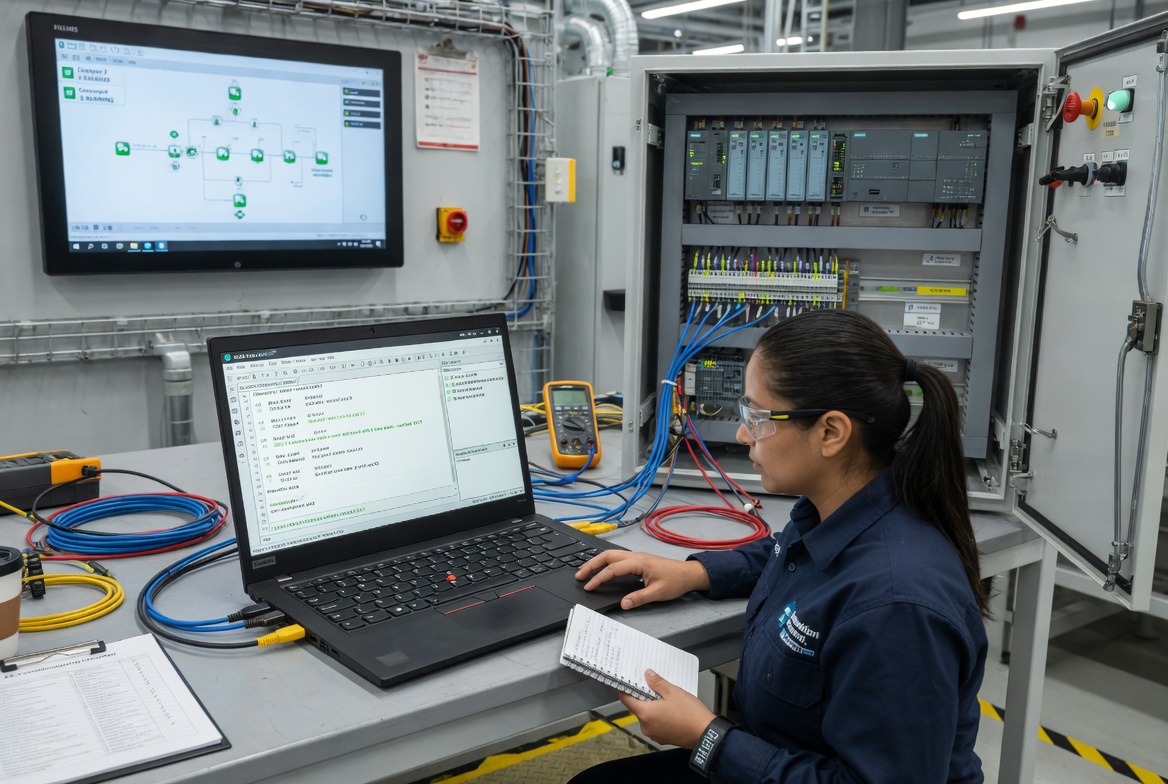
Custom AC500 PLC & Logic Programming
Turnkey software development engineered in ABB Automation Builder across modular AC500 V2 and V3 processors, delivering structured, maintainable code architectures for complex manufacturing processes.
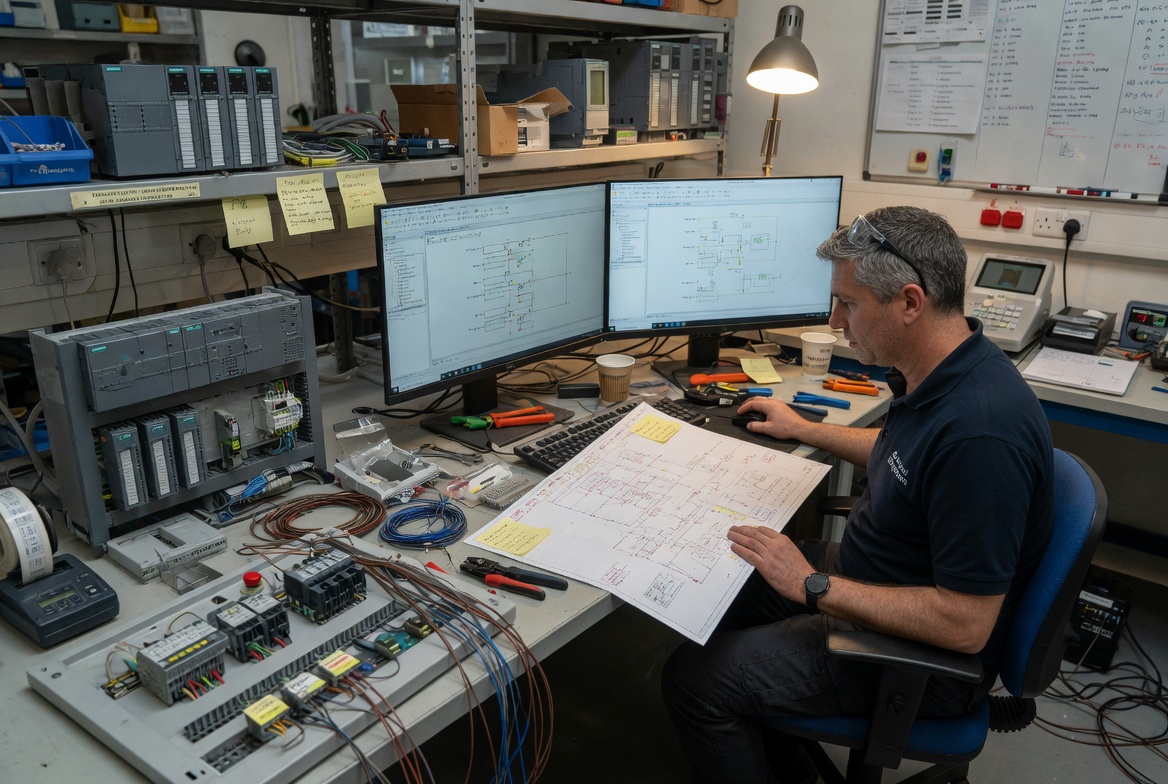
AC500-XC Extreme Condition Engineering
Specialized control engineering deploying ABB AC500-XC hardware for environments characterized by extreme cold, desert heat, severe mechanical vibration, high altitudes, and corrosive atmospheric gases.
AC500-S Functional Safety Integration
Engineering safety-critical control systems deploying ABB AC500-S certified safety PLCs, achieving SIL3 (IEC 62061) and Performance Level e (ISO 13849-1) compliance across machinery and material handling plants.
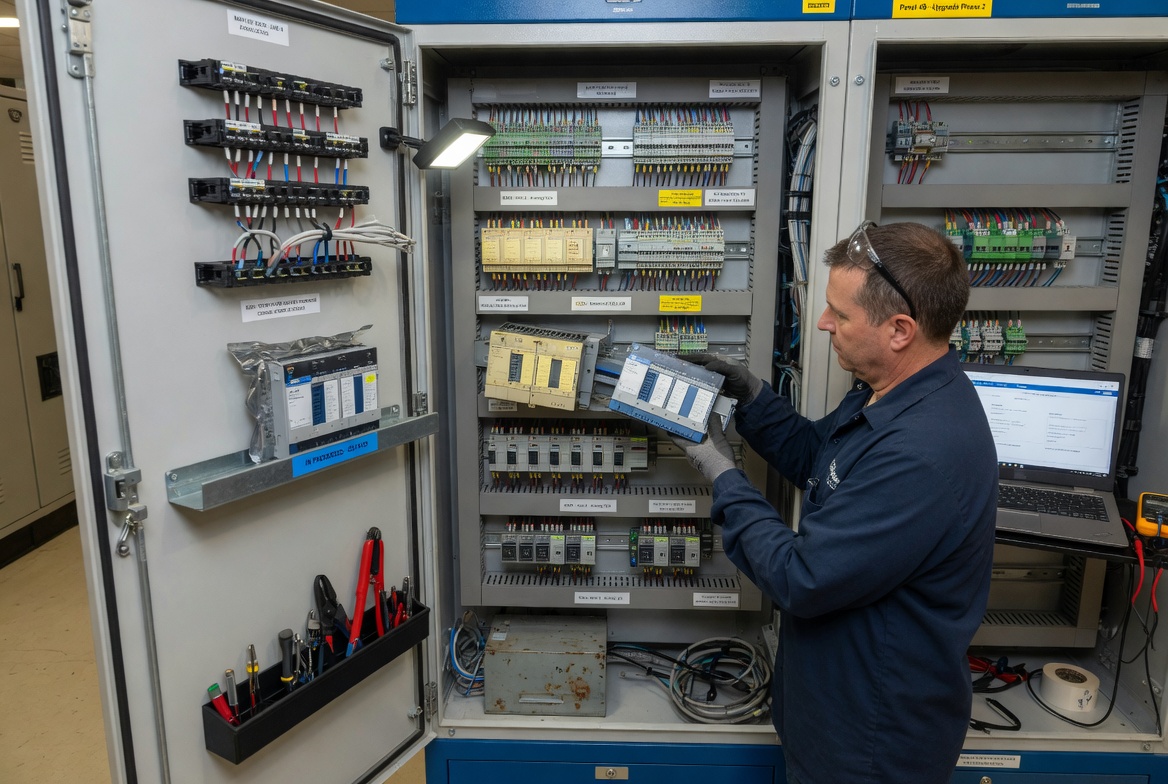
Multi-Protocol Networking & Telecontrol
Configuring robust industrial fieldbus backbones and telecontrol telemetry connecting ABB controllers directly with field devices, plant SCADA, and distributed utility monitoring networks.
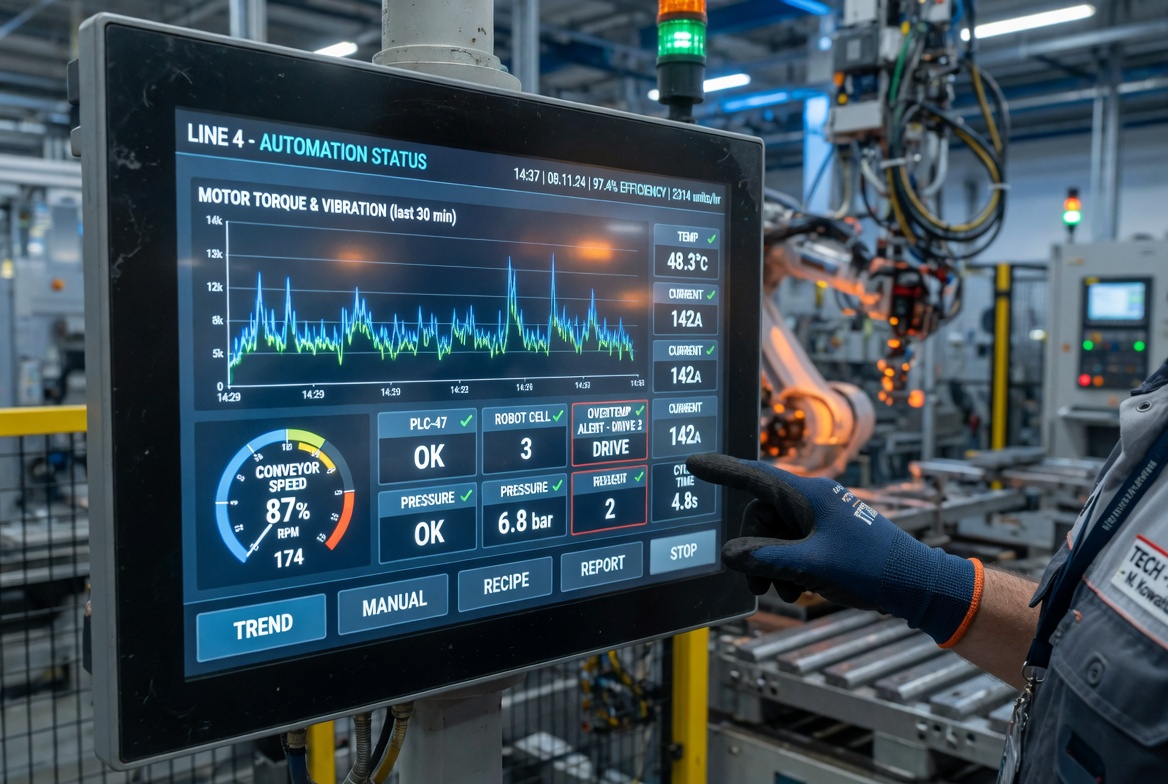
CP600 Touchscreen HMI & SCADA Systems
Designing responsive operator touchscreens on ABB CP600, CP600-eCo, and CP600-Pro terminals, delivering crystal-clear machine visualization, alarm management, and graphical historical trending.
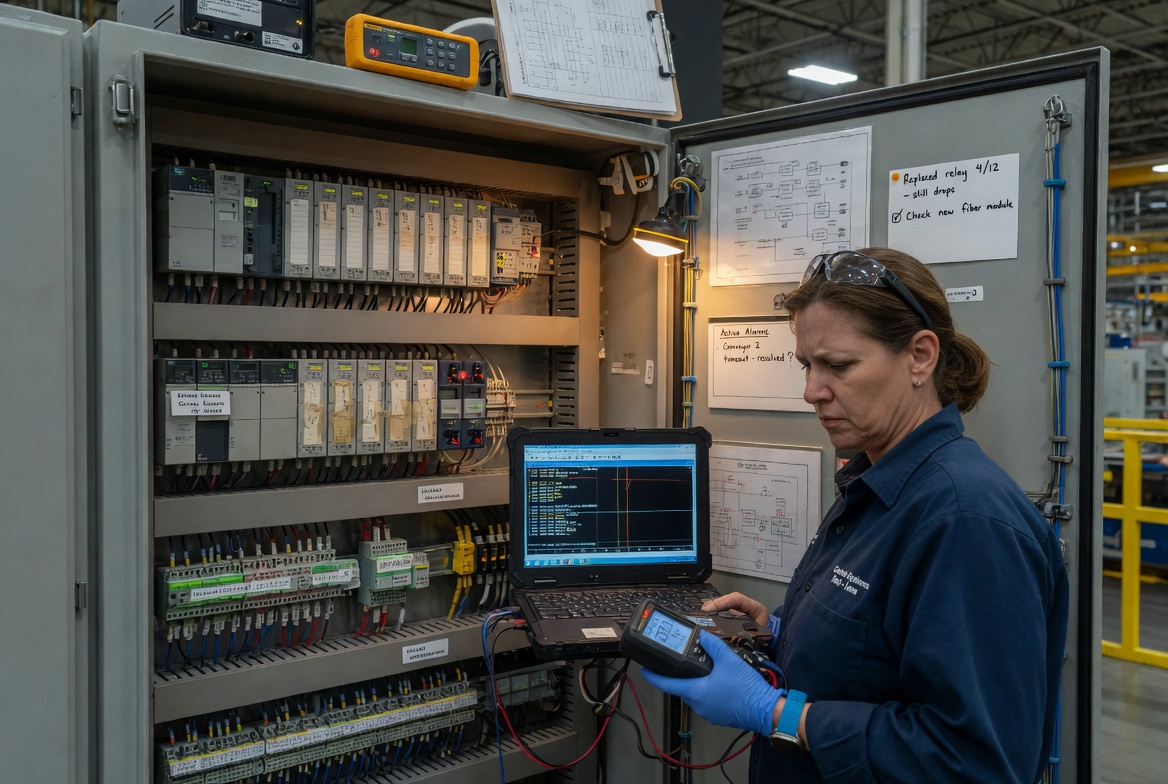
Diagnostics, Fault Finding & Breakdown Support
Rapid emergency on-site troubleshooting, communications analysis, and ongoing maintenance support for ABB automation platforms across the UK and worldwide.
Real-World Problems We Solve for ABB Automation Users
Plant engineers and infrastructure operators across the UK and worldwide trust MASK Control Systems to resolve persistent fieldbus faults, withstand harsh environments, and modernize legacy controllers.
Controller Failures in Extreme Environmental Conditions
Standard industrial PLCs suffering intermittent trips, board corrosion, or total failure when exposed to sub-zero cold, tropical heat, or corrosive chemical fumes.
We deploy ABB AC500-XC hardware with factory conformal coating, verified from -40 degrees C to +70 degrees C with 4g vibration resistance, ensuring perpetual plant reliability.
Protocol Incompatibility Across Mixed Field Devices
Machines requiring simultaneous communication with Profinet drives, Modbus flowmeters, and an OPC UA SCADA host, leading to fragmented wiring and external gateways.
We leverage AC500 modular communication cards to run up to four fieldbus protocols concurrently on one CPU, removing third-party gateways and reducing communication latency.
Complex and Hard-to-Maintain Safety Relay Panels
Industrial control cabinets crowded with dozens of hardwired safety relays, making fault finding during emergency stop trips time-consuming and prone to human error.
We integrate AC500-S safety controllers with PROFIsafe communications, delivering certified SIL3 / PL e machine protection alongside instantaneous diagnostic alarm readout on the HMI.
Discontinued Legacy Systems and Scarce Spares
Aging ABB MasterPiece, Advant Controller, or Procontic installations operating without spare parts, backup software archives, or modern network connectivity.
We modernize legacy software routines into structured Automation Builder projects and deploy pre-wired terminal adapters, executing changeovers during scheduled maintenance windows.
Unreliable Telemetry Communication to Central SCADA
Remote utility stations experiencing dropped connections, unbuffered historical logs, or security vulnerabilities when communicating over public cellular networks.
We configure native telecontrol protocols with time-stamped local event buffering, guaranteeing zero data loss during cellular interruptions and robust cyber security.
Our 6-Step ABB Automation Engineering Process
Every project follows our systematic engineering framework, from initial functional specification through to in-house panel testing and live site validation.
System Audit & Environmental Review
Thorough assessment of functional specifications, environmental severity (temperature, vibration, chemical exposure), and safety performance levels.
Hardware Architecture & Schematics
Developing complete ABB controller configurations, communication topologies, and BS EN 61439 electrical CAD schematics.
Software Engineering
Writing modular, documented PLC logic in Automation Builder alongside intuitive CP600 touchscreen operator screens.
In-House FAT Simulation
Rigorous offline simulation and Factory Acceptance Testing at our Devon panel workshop to verify every sequence before site delivery.
On-Site Commissioning & SAT
Physical machine testing, drive tuning, safety trip verification, and throughput optimization under live plant operating loads.
Handover & 24/7 Support
Complete As-Built documentation handover, source project archives, operator training, and ongoing SLA technical support.
Where Our ABB AC500 Solutions Are Deployed
We engineer ABB automation systems tailored to the exact regulatory and technical standards of your manufacturing or municipal infrastructure sector.
Water & Wastewater Infrastructure
Automated municipal pumping stations, aeration blower sequencing, chemical dosing skids, and IEC 60870-5-104 telecontrol integration.
Marine Vessels & Offshore Platforms
Engine telemetry, ballast control, winch monitoring, and auxiliary plant automation utilizing DNV-approved AC500-XC hardware.
Sub-Zero Cold Storage & Extreme HVAC
Refrigeration compressor sequencing, chiller plant management, and automated handling inside -40 degrees C deep-freeze logistics facilities.
Automated Cranes & Material Hoists
Heavy gantry cranes, container spreaders, and vertical freight lifts utilizing AC500-S functional safety and synchronized drive control.
Food, Beverage & Processing Skids
Clean-in-place (CIP) washdown manifolds, recipe batch dosing, pasteurisation controls, and hygienic conveyor sorting lines.
Special Purpose Machinery & Test Stands
Bespoke production machinery, automated hydraulic test benches, rotary indexing tables, and multi-station assembly cells.
Frequently Asked Questions
Clear answers regarding our ABB AC500 PLC programming, extreme environmental hardware, and telecontrol integration services.
Q:Which ABB PLC hardware ranges do you program and support?
We support the entire ABB PLC ecosystem, including the flagship modular AC500 V2 and V3 controllers, cost-effective AC500-eCo standalone micro PLCs, AC500-XC extreme environment controllers, and AC500-S functional safety PLCs (SIL3 / PL e), alongside S500 distributed slice I/O modules.
Q:What makes the ABB AC500-XC suitable for harsh and marine environments?
The AC500-XC (eXtreme Conditions) platform is factory-hardened for operating temperatures from -40 degrees C to +70 degrees C, 4g continuous vibration resistance, altitudes up to 4,000 meters, and resistance to corrosive industrial gases (ISA S71.04 severity level G3) and saltwater spray, making it ideal for offshore marine and chemical installations.
Q:What programming languages do you use within ABB Automation Builder?
Using ABB Automation Builder, which is built on the industry-standard CODESYS v3 platform, we program in all five IEC 61131-3 languages: Structured Text (ST), Ladder Diagram (LD), Function Block Diagram (FBD), Continuous Function Chart (CFC), and Sequential Function Chart (SFC).
Q:Can an ABB AC500 controller bridge multiple industrial fieldbuses at once?
Yes. ABB AC500 CPUs feature modular communication interface slots that allow up to four different network protocols to run simultaneously on a single controller, enabling seamless multi-protocol bridging between Profinet, Modbus TCP, EtherCAT, CANopen, and Profibus DP without external hardware gateways.
Q:Do you support telecontrol protocols like IEC 60870-5-104 for water and utilities?
Yes. We configure native telecontrol protocols including IEC 60870-5-104, DNP3, and Modbus TCP for municipal pumping stations, wastewater treatment plants, and electrical distribution substations, integrating directly with regional SCADA monitoring centres.
Q:Where do you provide on-site engineering and emergency breakdown support?
Our engineering headquarters and BS EN 61439 control panel manufacturing workshop are based in Cullompton, Devon. We provide rapid on-site emergency troubleshooting across the UK as well as international remote support and commissioning worldwide.
Why Choose MASK Control Systems for Your ABB Projects
We are not just programmers; we are turnkey control systems engineers with our own dedicated panel manufacturing facility in Cullompton, Devon. We design, build, test, and commission complete systems with absolute accountability.
Need Expert ABB AC500 PLC Programming or Migration Support?
Whether programming an extreme-environment AC500-XC installation, commissioning an AC500-S functional safety system, or resolving an urgent breakdown, our engineers are ready to support your operations.